 中铸智能ZOOMZU
Get a quote
中铸智能ZOOMZU
Get a quote
From layout design and equipment selection to installation, commissioning and operator training — one team responsible for the whole line, so your foundry starts producing on schedule.
Top & bottom or side shooting; mould hardness 85–95 B.
Transfer cars and pouring equipment synchronized with cooling.
Cooling tunnel controls shakeout temperature and takt.
Vibrating shakeout separates castings and sand.
Surface cleaning removes sand and oxide skin.
Used sand treated and returned to the loop.
Reclamation, mixing, moisture and temperature control.
* Indicative schedule; actual timing depends on project scope, configuration and site conditions.
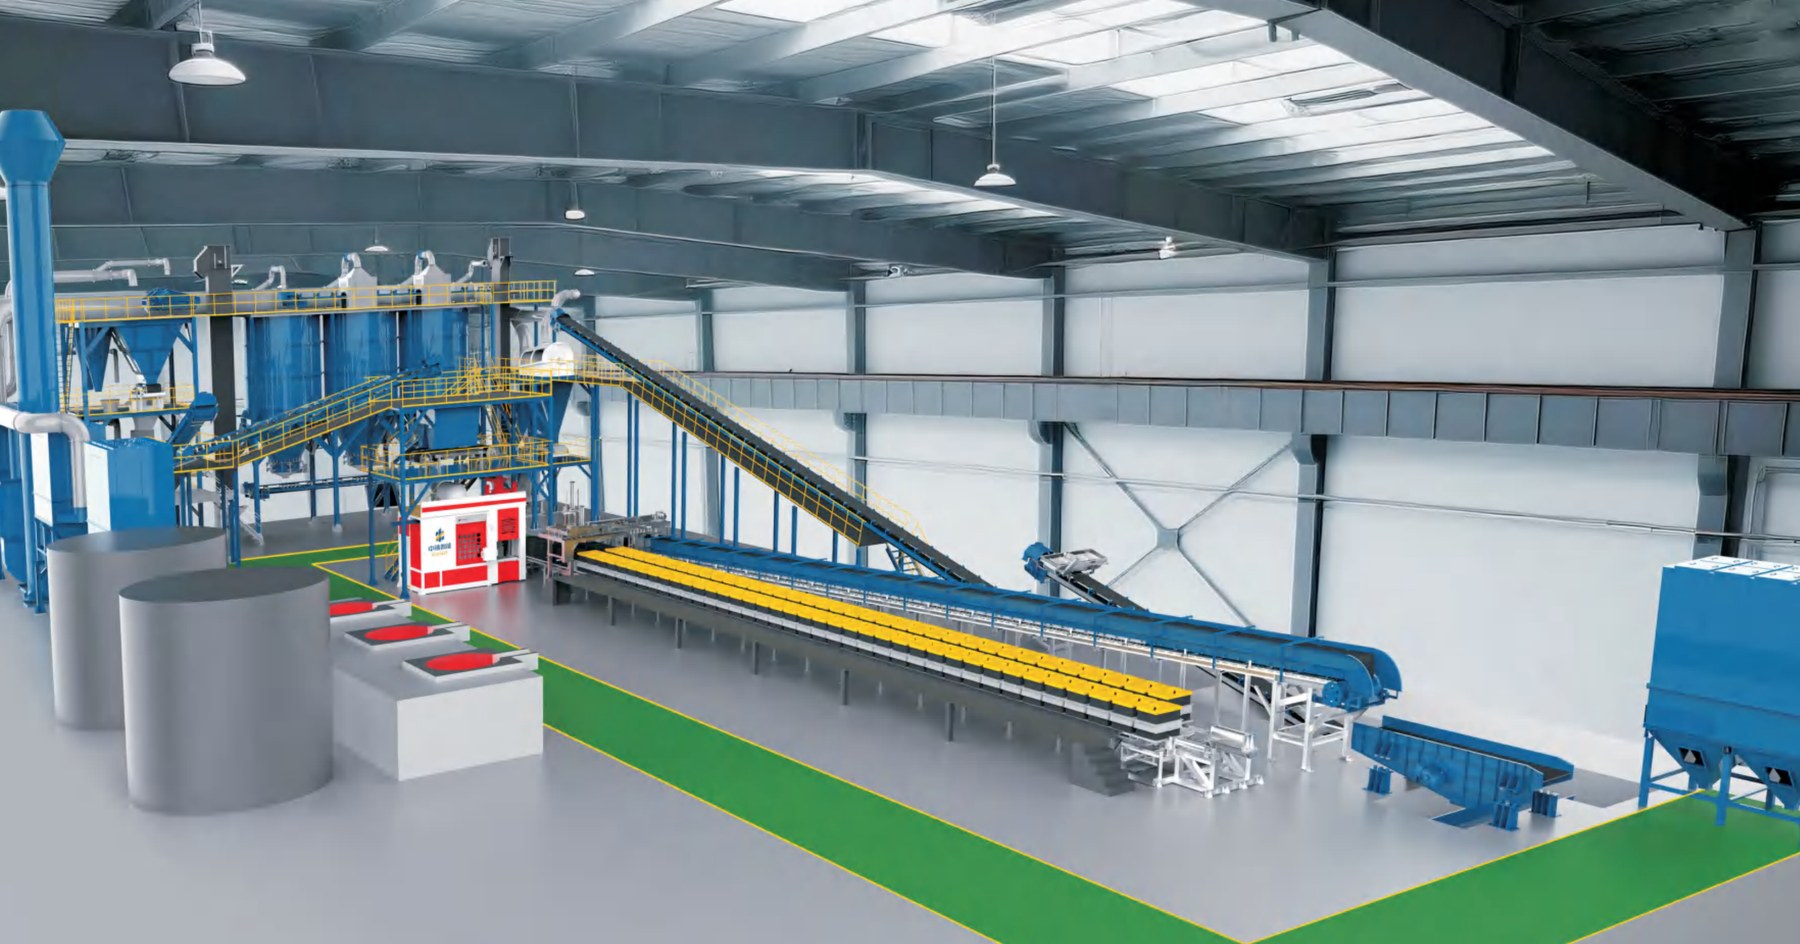
Plant layout based on building size, output target and casting mix, with maintenance and logistics access.
Moulding, sand, pouring, cooling and blasting matched in interface and takt.
On-site installation, linked commissioning and trial production until mould quality and takt are met.
Operator and maintenance training, spare parts and remote support for long-term uptime.
Casting types, output target, existing plant and budget.
1–2 weeksLayout, equipment list, takt calculation and investment estimate.
2–4 weeksEquipment manufacturing, factory testing and pre-acceptance.
10–16 weeksOn-site installation, linked commissioning and trial production.
4–8 weeksOperator training, spare parts and remote support.
Ongoing* Indicative schedule; actual timing depends on project scope, configuration and site conditions.